Commercial Vacuum Packing Machine

Ultimate Freshness & Preservation: With a robust 100 - 150W motor and 2000mL+ vacuum capacity, this sealer removes air in seconds,
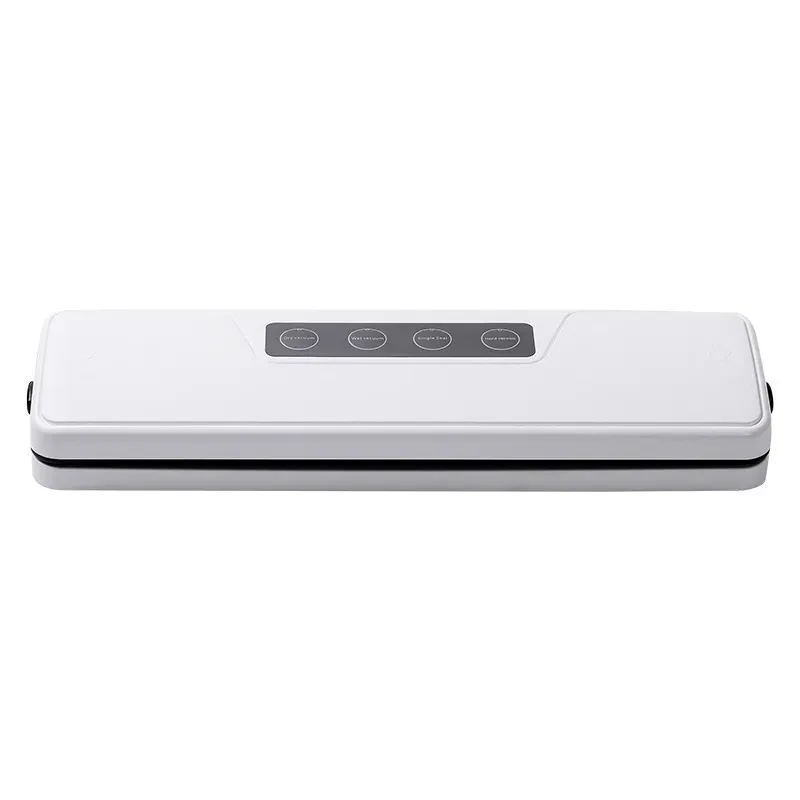
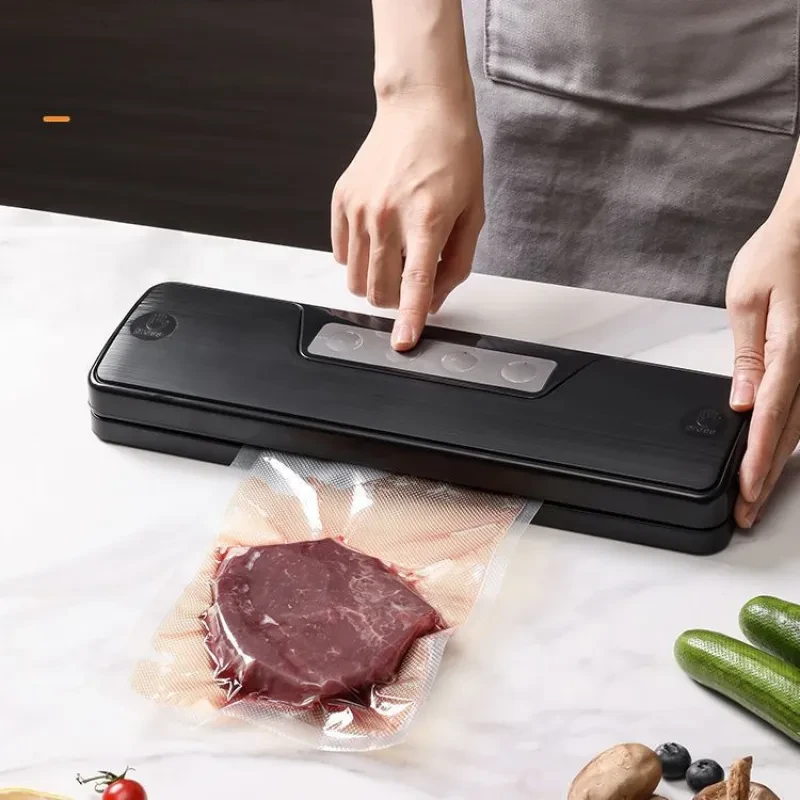
locking in freshness for meats, veggies, fruits, and leftovers. The one - touch operation (as shown in the image) makes it effortless to
seal, extending food shelf life and preventing freezer burn.
Durable & Safe Design: Crafted from high - quality ABS material, it’s lightweight, impact - resistant, and easy to clean. The included
10 food - grade vacuum bags (17×25cm) are BPA - free, perfect for storing, marinating, or sous vide cooking.
Global Compatibility & Versatility: Designed for worldwide use (100 - 240V), it’s ideal for households, small kitchens, or outdoor
adventures. Use it to preserve snacks, seal coffee beans, or organize pantry items – a must - have for zero - waste living!
Commercial Vacuum Packing Machine – High-Performance Food Sealing Solution
Perfect for Restaurants, Butchers, Food Producers, and Commercial Kitchens
The commercial vacuum packing machine is designed for high-volume food preservation and professional packaging environments where freshness, hygiene, and shelf-life extension are critical. It is widely used in restaurants, butcher shops, supermarkets, catering services, and food production facilities that require consistent sealing performance and reliable operation throughout the day.
This machine is ideal for businesses that need to reduce food waste, maintain product quality, and improve storage efficiency. Whether sealing fresh meat, seafood, dry goods, or prepared meals, it delivers strong vacuum pressure and airtight sealing to protect contents from oxidation, moisture, and contamination.
Description – Commercial Vacuum Packing Machine
A commercial vacuum packing machine is a heavy-duty food preservation device that removes air from specially designed vacuum bags and seals them tightly to create an airtight environment. This process significantly extends shelf life by slowing bacterial growth and preventing freezer burn or spoilage.
Built for continuous use, the machine typically features a durable stainless-steel body, a powerful vacuum pump, and an adjustable sealing system. These components ensure consistent performance even under demanding commercial workloads.
Most units include multiple operating modes such as automatic vacuum sealing, manual control for delicate foods, and adjustable sealing time settings. This allows operators to handle a wide variety of food textures, from soft bakery items to dense cuts of meat.
The sealing bar is engineered for precision, ensuring a strong and uniform seal across every bag. This reduces the risk of leakage during storage or transport. Many models also support external vacuum canisters and roll storage systems for added flexibility in packaging options.
Designed with efficiency in mind, the machine helps streamline kitchen workflows. Food can be pre-portioned, sealed, and stored in bulk, improving inventory control and reducing daily preparation time.
Key Points
Heavy-Duty Vacuum System: Equipped with a powerful pump that efficiently removes air to create a tight vacuum seal suitable for commercial workloads.
Stainless Steel Construction: Built with durable materials that resist corrosion, heat, and frequent cleaning in professional kitchen environments.
Adjustable Sealing Control: Allows operators to control sealing time and pressure for different food types, ensuring safe packaging for both delicate and dense products.
Multi-Purpose Usage: Suitable for sealing meat, seafood, vegetables, dry goods, prepared meals, and sous-vide portions.
Benefits
The main benefit of a commercial vacuum packing machine is extended food shelf life. By removing oxygen, it significantly slows down spoilage and preserves freshness for longer periods compared to standard storage methods.
It also improves cost efficiency by reducing food waste. Businesses can buy in bulk, portion ingredients in advance, and store them safely without rapid deterioration.
Another advantage is improved hygiene and food safety. Airtight packaging prevents contamination from external elements such as moisture, dust, and bacteria.
Operational efficiency is also enhanced, as staff can prepare and package food in advance, reducing pressure during peak service hours.
Why You Choose This
This machine is chosen by professional kitchens because it delivers consistent, industrial-grade performance without complicated operation. It is designed for reliability, making it suitable for daily use in high-demand environments.
Its versatility makes it a practical investment for multiple industries, from hospitality to retail food packaging. The ability to handle both wet and dry foods adds flexibility to business operations.
Additionally, its durable construction ensures long-term use with minimal maintenance, making it a cost-effective solution for businesses focused on efficiency and scalability.
Conclusion
The commercial vacuum packing machine is an essential tool for any food-related business that values freshness, efficiency, and professional packaging standards. It helps extend product shelf life, reduce waste, and improve overall kitchen workflow. With strong sealing performance and durable construction, it is built to support continuous commercial use and deliver reliable results every time.
The product may be provided by a different brand of comparable quality.
The actual product may vary slightly from the image shown.
Shop amazing plants at The Node – a top destination for plant lovers